English

Looking for factory-direct figures before getting lost in hundred-page technical brochures? Direct wholesale gate pricing for genuine P0.9 Micro/Mini LED video walls from specialized cleanroom factories in Shenzhen and Huizhou ranges from $7,500 to $12,500 per square meter, depending strictly on whether you specify Full Flip-Chip COB (Chip-on-Board) or discrete MIP (Micro LED in Package) diodes. Sourcing directly from verified Tier-2 cleanroom OEM plants saves commercial AV integrators and commercial builders 45% to 60% compared to Western turnkey enterprise brands, but you have to mandate common-cathode 2.8V/3.8V dual-rail power and factory-archived color calibration profiles to avoid catastrophic dead-pixel replacement headaches later on.
When people search for wholesale p0.9 led display manufacturers, they usually have an executive boardroom, private screening room, or high-security monitoring center project where a standard 1.2mm or 1.5mm screen simply isn't sharp enough. But stepping down into sub-1mm territory is a completely different ballgame. At P0.9375, you are packing approximately 1,230,000 pixels into a single square meter. That means more than 3.6 million microscopic red, green, and blue semiconductor chips humming away in an area barely the size of an office desk.
If an OEM cuts corners on cleanroom SMT placement, thermal dissipation, or forward-voltage binning, that wall will start dropping sub-pixels within months. How do you find a factory that actually has the equipment to build reliable sub-1mm video walls without paying a 300% corporate markup? Let's take a look under the hood.
If a sales representative sends you a quote for a "P0.9 SMD display," close the chat window immediately.
Traditional Surface Mounted Device (SMD) packaging maxes out around P1.2. Below 1.0mm, the solder pads for individual diode packages are so microscopic that surface tension during reflow soldering causes the diodes to twist, lift, or break off at the slightest touch.
When sourcing from legitimate wholesale p0.9 led display manufacturers today, you are choosing between three specific architectural approaches:
[Silicon Wafer Processing]
           │
           ├───────────────────────────────┬───────────────────────────────┐
           ▼                               ▼                               ▼
 [Full Flip-Chip COB]                 [MIP Packaging]               [IMD / 4-in-1 Matrix]
  • Bare dies bonded direct to PCB     • Discrete Micro-SMD diodes   • Four pixels grouped in 1 case
  • Seamless resin protective flood    • SMT-compatible placement    • Transitional legacy tech
  • High contrast, ultra-durable       • Easy single-pixel rework    • High solder joint stress
Full Flip-Chip COB (Chip-on-Board): Bare semiconductor dies are flipped upside down and bonded directly to the PCB circuit traces with no wire bonding. The entire module face is then sealed in an optically clear, matte-black epoxy or polyurethane resin. It is completely flat, dustproof, and moisture-resistant. This is the premier standard for P0.9 enterprise installations.
MIP (Micro LED in Package): Micro-scale semiconductor chips are pre-packaged into microscopic standalone carriers (like 0404 or 0202 packages) with pre-tested optical binning, then placed on standard high-precision SMT lines. MIP allows individual pixel testing before mounting and makes field repair easier, though black-level uniformity across wide viewing angles requires strict mask tolerances.
IMD (Integrated Matrix Devices / 4-in-1): An older transitional technology where four pixels are grouped into a single surface-mount package. Say what you will about early adoption, but IMD was a stepping stone. In sub-1mm applications, IMD packages still suffer from mechanical solder-pad strain and noticeable seam lines, which is why modern high-spec projects have largely migrated away from it.
To make the right hardware trade-off for your installation site, here is how the primary packaging methods stack up against each other:
| Key Technical Parameter | Full Flip-Chip COB | MIP (Micro LED in Package) | IMD (4-in-1 Matrix) |
|---|---|---|---|
| Surface Physical Protection | IP65 Front (Waterproof, Impact-proof) | IP40 (Bare diodes, GOB coating optional) | IP30 / IP40 (Fragile surface corners) |
| Field Service & Repairability | Factory cleanroom hot-tweezer rework | Standard on-site micro-soldering rework | Standard hot-air rework station |
| Contrast Ratio & Deep Blacks | Up to 20,000:1 (Deep matte-black resin) | 8,000:1 – 12,000:1 | 5,000:1 – 8,000:1 |
| Thermal Dissipation Path | Direct PCB substrate contact (Cool face) | Heat passes through package lead frames | Heat builds up inside quad-package |
| Off-Axis Color Uniformity | Superior (Near 170° viewing angle) | Very Good | Moderate (Color shift past 130°) |
| Average Production Cost Index | Premium (High upfront cleanroom tooling) | Moderate to High | Budget to Moderate |
Pricing on P0.9 display hardware changes quickly, but component realities keep baseline costs within predictable ranges. If someone quotes you $3,500/m² for a P0.9 display, you can bet your bottom dollar they are quoting non-flip-chip b-stock dies or clearance IMD modules that will fail their first thermal run.
Here are the real wholesale numbers for genuine grade-A P0.9 hardware sourced directly from mid-to-large Chinese manufacturers:
| Display Configuration | Typical Substrate / Cabinet | Average Factory Wholesale Price (USD/m²) | Critical Quality Metric | Best Application Environment |
|---|---|---|---|---|
| P0.9375 Full Flip-Chip COB | 600×337.5mm Die-Cast Aluminum | $8,800 – $12,500 / m² | Full black resin encapsulation, >15,000:1 | Corporate Boardrooms, Broadcast Studios |
| P0.9375 MIP Display | 600×337.5mm Magnesium Alloy | $7,800 – $10,500 / m² | Pre-sorted binning, matte mask | Luxury Home Cinemas, Higher Ed Labs |
| P0.9 Micro LED Ultra-Fine | 640×360mm Precision CNC Frame | $11,500 – $15,000 / m² | Common-cathode driver, DCI-P3 98% | Command & Control, Defense Simulators |
| P1.25 Flip-Chip COB (Reference) | 600×337.5mm Aluminum Frame | $4,200 – $5,800 / m² | Proven 2-year field stability | High-end Conference Rooms |
Note: Pricing reflects raw screen cabinets, standard receiving cards, and basic magnetic mounting brackets. High-end video processors (NovaStar MX40 Pro, Brompton SX40), structural framing, international shipping, and customs tariffs are separate line items.
Here is a detail that trips up a lot of AV project managers: resolution density.
On a standard P2.5 screen, building a native 4K canvas (3840×2160 pixels) requires a screen roughly 31.5 feet wide by 17.7 feet tall (9.6m × 5.4m). That is a massive wall.
On a P0.9375 display, building that exact same native 4K canvas requires a screen that is only 11.8 feet wide by 6.6 feet tall (3.6m × 2.0m).
[Standard 16:9 Display Canvas Size Comparison for Native 4K UHD]

P2.5 Display Wall:  [ 31.5 ft Wide x 17.7 ft High ] ──> ~557 sq ft (Huge auditorium)
P1.25 Display Wall: [ 15.7 ft Wide x 8.8 ft High  ] ──> ~138 sq ft (Large conference room)
P0.93 Display Wall: [ 11.8 ft Wide x 6.6 ft High  ] ──> ~78 sq ft  (Standard executive office wall)
Because you are packing millions of pixels into a tight footprint, your video transmission pipeline faces extreme data pressure:
A single 1Gbps Ethernet data port on a traditional controller only handles roughly 650,000 pixels at 60Hz 8-bit.
A native 4K canvas contains roughly 8.3 million pixels.
That means you need at least 13 to 14 dedicated Gigabit Ethernet lines running to a screen that is only twelve feet wide.
This is why leading wholesale p0.9 led display manufacturers have transitioned to 5G transmission protocols (such as NovaStar's COEX platform paired with Armor A10s Pro or CA50 receiving cards). With 5G transmission lines, a single cable carries over 2.6 million pixels, reducing the messy tangle of Cat6 cables behind your wall by more than 70%.
When drafting your supplier specs, verify whether their receiving cards support 5G serialization. If they are still using standard 1G cards, your installers will have to run dozens of delicate patch cables through cramped cabinet cavities.
Have you ever stood in front of a fine-pitch video wall and felt heat radiating onto your face like an open toaster? That happens when a manufacturer uses conventional Common Anode (5V) circuits.
In an ultra-fine P0.9 matrix, that amount of thermal buildup is lethal to the electronics. Diodes that stay overheated suffer rapid lumen depreciation, and the PCB substrate expands slightly. In a P0.9 display, a thermal expansion of just 0.08mm across a cabinet edge will push adjacent pixels together, creating glaring, bright seam lines that ruin the visual presentation.
Conventional Common Anode (High Thermal Load):
[Single 5V DC Rail] ──┬──> Red Diode   (Needs ~2.1V; 2.9V wasted as HEAT)
                      ├──> Green Diode (Needs ~3.2V; 1.8V wasted as heat)
                      └──> Blue Diode  (Needs ~3.2V; 1.8V wasted as heat)
                      *Result: Surface runs hot (~50°C+), diodes degrade quickly.

Advanced Common Cathode (Low Thermal Load):
[2.8V DC Rail] ──────────> Red Diode   (Needs ~2.1V; minimal waste heat)
[3.8V DC Rail] ───────┬──> Green Diode (Needs ~3.2V; minimal waste heat)
                      └──> Blue Diode  (Needs ~3.2V; minimal waste heat)
                      *Result: Surface stays cool (~35°C), long lifespan, zero expansion.
When talking with factory engineers, make Common Cathode an absolute requirement:
By feeding 2.8V DC to the red chips and 3.8V DC to the green and blue chips, overall display power consumption drops by 25% to 35%.
The screen face stays comfortably cool (around 32°C to 36°C), which is essential if executives are sitting four feet away in an air-conditioned boardroom.
Thermal expansion is virtually eliminated, keeping seams invisible across seasonal temperature shifts.
Shenzhen's Bao'an and Guangming districts house hundreds of LED companies, but only a fraction have the specialized cleanroom infrastructure needed to manufacture reliable sub-1mm COB modules.
A standard workshop with open assembly lines, ceiling fans, and hand-held soldering irons cannot build P0.9 panels. A single speck of airborne dust landing on a bare silicon pad before the epoxy potting cure will cause an open circuit or permanent color short.
                      [Sourcing Verification Flow]
                                   │
      ┌────────────────────────────┴────────────────────────────┐
      ▼                                                         ▼
[Class 1000 / Class 100 Cleanroom]                 [Standard Commercial Assembly Floor]
  • Automated AGV wafer handling                     • Manual worker component handling
  • ASM / Kulicke & Soffa die-bonders                • Open air environment (dust risks)
  • 3D SPI and X-Ray BGA inspection                  • Visual inspection with magnifying glass
  • True COB / Micro-LED Factory                     • Trading Company / Downstream Assembler
If you plan to audit a prospective factory in China—or hire a third-party inspection agency like SGS to conduct the audit—verify these specific hardware milestones on the manufacturing floor:
Cleanroom Classification: The die-bonding and resin-packaging lines must operate within a certified Class 1000 (ISO 6) or Class 100 cleanroom environment. Workers must wear full anti-static cleanroom bunny suits, pass through air showers, and use automated material handling.
High-Speed Die-Bonding Machinery: Look for automated die-bonding equipment from recognized global toolmakers like ASM Pacific, Kulicke & Soffa (K&S), or Besi. These machines use optical alignment systems to pick up bare micro-dies from silicon wafers and place them onto the PCB substrate with positional tolerances under 3 microns.
Automated Optical & X-Ray Inspection: Because you cannot inspect microscopic flip-chip solder joints with the naked eye, a qualified cleanroom must use 3D Solder Paste Inspection (SPI) before placement and automated X-ray inspection (AXI) after reflow. This checks for hidden voids, micro-bridging, or insufficient wetting beneath the chips.
72-Hour Continuous Low-Grayscale Aging: Every manufacturer runs full-white burn-in, but the real test for P0.9 is low-brightness flat gray (10% to 15% luminance). Ask the factory to show you their dark aging room. If modules can display a solid, perfectly uniform dark-gray screen across 50 panels without blotchiness, pink clouds, or dead sub-pixels, their binning algorithms and driver calibrations are solid.
This is the number one concern for first-time COB buyers. Because the face of a COB panel is coated in a continuous resin shield, you cannot simply take a standard soldering iron and swap out an individual diode on the job site.
Here is how maintenance actually works:
Module Swapping: Every commercial P0.9 system is built with front-service magnetic retention. If a pixel fails, a technician uses an electro-vacuum extraction tool to safely pop the entire 150×168.75mm module forward off the cabinet chassis in under 15 seconds. You plug in a matching spare module from your attic stock, and the screen is back in service immediately.
Factory Cleanroom Rework: The defective module is placed into anti-static protective foam and shipped back to the manufacturer (or a certified regional repair hub). Technicians use precision laser ablation to remove the local resin shield, replace the micro-die using microscopic hot-tweezers under a digital microscope, and apply a factory resin patch.
Because on-site diode repair isn't practical, you must order 8% to 12% matching spare modules from the exact same production lot upfront.
On a standard P3.9 outdoor screen, if you swap in a module from a different batch, the slight color variation is often masked by high brightness and viewing distance. On a P0.9 indoor screen viewed from five feet away, even a 1.5nm dominant wavelength variance or a 2% forward-voltage difference between batches will stand out like an obvious stain.
Always require the manufacturer to provide:
The original Receiving Card Configuration File (.rcfgx / .rcg).
The raw CCD camera calibration coefficient data table archived on a secure cloud link.
Written documentation that all spare modules in your crate were packaged using the same wafer lot and resin potting run.
For fine-pitch indoor walls, cabinet rigidity is critical. A standard sheet-metal chassis is completely unsuitable here.
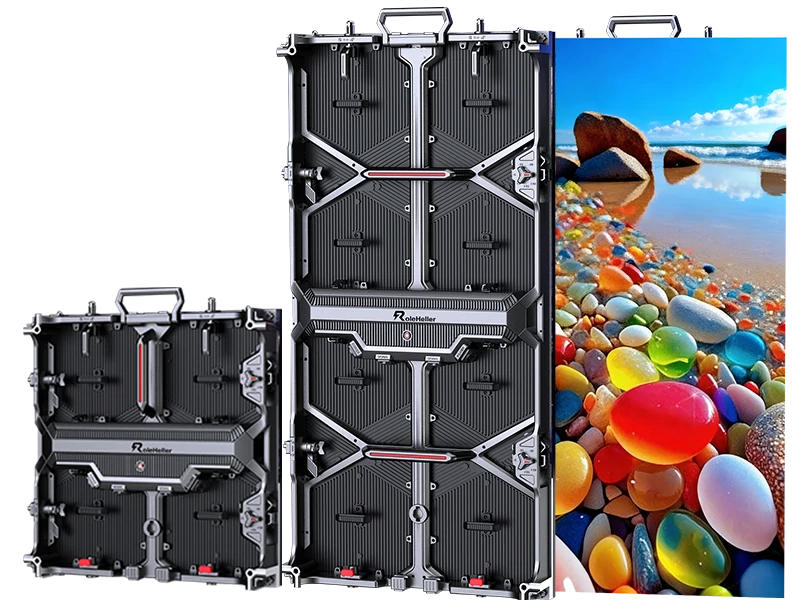
CNC Die-Cast Aluminum (600×337.5mm): The industry workhorse. Die-cast frames are machined on high-precision CNC multi-axis milling centers to achieve dimensional tolerances within ±0.03mm. Aluminum provides high structural rigidity and acts as a natural heat sink.
Magnesium Alloy: Approximately 30% lighter than aluminum, making it easier to handle during installation. However, magnesium has a slightly higher thermal expansion coefficient and requires strict torque calibration during bolt-up to avoid micro-twisting the chassis.
For permanent high-end indoor installations, precision CNC aluminum remains the more reliable choice.
Having overseen numerous fine-pitch LED installations, a few hard-won lessons are worth keeping in mind:
First, don't over-specify resolution if the physical space doesn't demand it. A native 4K P0.9 display is only about twelve feet wide. If your conference room has viewers sitting ten to fifteen feet back from the screen, a high-quality P1.25 flip-chip COB display will look just as crisp to the human eye, run cooler, and save you 40% on your hardware budget. Choose P0.9 when viewers are sitting within three to six feet (1 to 2 meters) of the display, such as in control rooms or intimate executive suites.
Second, pay close attention to your room's acoustic and thermal profile. P0.9 displays draw substantial power when displaying full-white spreadsheets or presentation slides. If you pack thirty cabinets into a small conference room without adequate HVAC airflow, the ambient room temperature will rise noticeably. Choose common-cathode hardware and make sure your mechanical engineers account for the display's thermal BTU output.
Third, make sure the manufacturer includes a specialized electro-vacuum extraction tool in the shipment. Never let an installer attempt to pry off a fine-pitch module using plastic pry tools or flathead screwdrivers. One slip against the edge of a P0.9 module can shatter dozens of micro-diodes along the seam, turning an expensive panel into salvage.
Approach your procurement process with clear technical requirements. Spell out cleanroom standards, mandate common-cathode drivers, verify 5G receiving card compatibility, and secure adequate spare modules upfront. Taking these steps will help you build a clean, reliable, ultra-fine-pitch video wall that performs flawlessly for years.
The general rule of thumb for comfortable viewing distance is roughly 1 meter per millimeter of pixel pitch. For a P0.9375 display, the minimum comfortable viewing distance is 3 to 4 feet (0.9 to 1.2 meters). At this distance, the human eye cannot resolve individual pixels, and content appears completely smooth and filmic, similar to an OLED panel.
A native 4K canvas at P0.9375 measures approximately 11.8ft × 6.6ft (roughly 7.2 square meters). At factory wholesale hardware rates of $8,500 to $11,000 per square meter, the bare display hardware runs between $61,000 and $79,000. Adding high-end video processing (such as a NovaStar MX40 Pro), structural mounting brackets, audio, freight, and installation typically brings the total project cost to $85,000 – $115,000. This is significantly lower than retail turnkey brand pricing, which often exceeds $200,000.
Yes, P0.9 flip-chip COB displays are well-suited for high-end residential private cinemas. Because COB panels have a matte-black resin face, they deliver contrast ratios exceeding 15,000:1 and deep black levels that approach OLED quality, while producing 600 to 1,000 nits of peak HDR brightness without the projector washout common in ambient room light.
The difference comes down to the microscopic size of the semiconductor die: Mini LED diodes typically measure between 100 and 200 microns in size, whereas Micro LED diodes measure under 50 microns. True Micro LED dies provide wider spacing between emitters on the substrate, allowing for deeper black epoxy backgrounds, higher contrast, and improved power efficiency, whereas Mini LED represents an intermediate step.
Quality P0.9 displays built with full flip-chip dies and common-cathode circuitry carry an engineering rating of 100,000 hours of operational life. In real-world commercial environments running 12 hours a day at 50% to 60% calibrated brightness, you can realistically expect 10 to 12 years of reliable performance before diode lumen depreciation or driver component aging becomes noticeable.
Traditional SMD displays at sub-1.5mm pitches are fragile and prone to edge-chipping. However, Full Flip-Chip COB displays are physically durable. Because the diodes are embedded within an optically clear resin shield, the face can withstand accidental finger pokes, cleaning with a microfiber cloth, and mild surface impacts without diode loss. The edges remain the only sensitive zone during cabinet assembly.
For fine-pitch P0.9 projects, NovaStar's COEX platform (processors like the MX30 or MX40 Pro paired with CA50/Armor receiving cards) or Brompton Technology (Tessera SX40) are the leading choices. They provide 12-bit to 16-bit low-grayscale processing, full HDR10/HLG color profiles, low latency, and 5G bandwidth capabilities essential for sub-1mm resolutions.
At maximum white screen load, a P0.9 display typically draws 500W to 700W per square meter. During normal real-world video playback (corporate presentations, movies, dashboards), average power consumption drops to roughly 180W to 250W per square meter. A standard 4K wall (7.2 m²) will draw roughly 1.3kW to 1.8kW average, which can be powered from standard 20A dedicated commercial circuits.
Most fine-pitch displays are mounted directly against structural drywall or recessed into custom architectural millwork. Front-service magnetic modules allow technicians to access power supplies, receiving cards, and display modules directly from the front using a vacuum tool, eliminating the need to build an expensive, space-wasting rear service corridor behind the display.
Fine-pitch displays ship in heavy-duty wooden crates or flight cases lined with custom CNC-cut EVA high-density foam. Most overseas buyers without an in-house customs broker purchase under DDP (Delivered Duty Paid) terms. Under DDP, the manufacturer's logistics freight forwarder handles export clearance, air or ocean transit, customs brokerage, import duties, and lift-gate delivery directly to your facility door.